Vistanut International
Premium Cashews
Visual breakdown of our industrial cashew processing pipeline from farmgate orchard harvest to nitrogen vacuum packaging. Click on any stage card to inspect machine calibrations, thermal parameters, and QA protocols.
Total Workflow
11 Sequential Stages
KOR Quality
48 - 52 lbs / Bag
Thermal Boiling
90°C Micro-Pressure
Whole Kernel Yield
>94% Intact Recovery
Vacuum Sealing
<0.5% Residual Oxygen
 STAGE 01
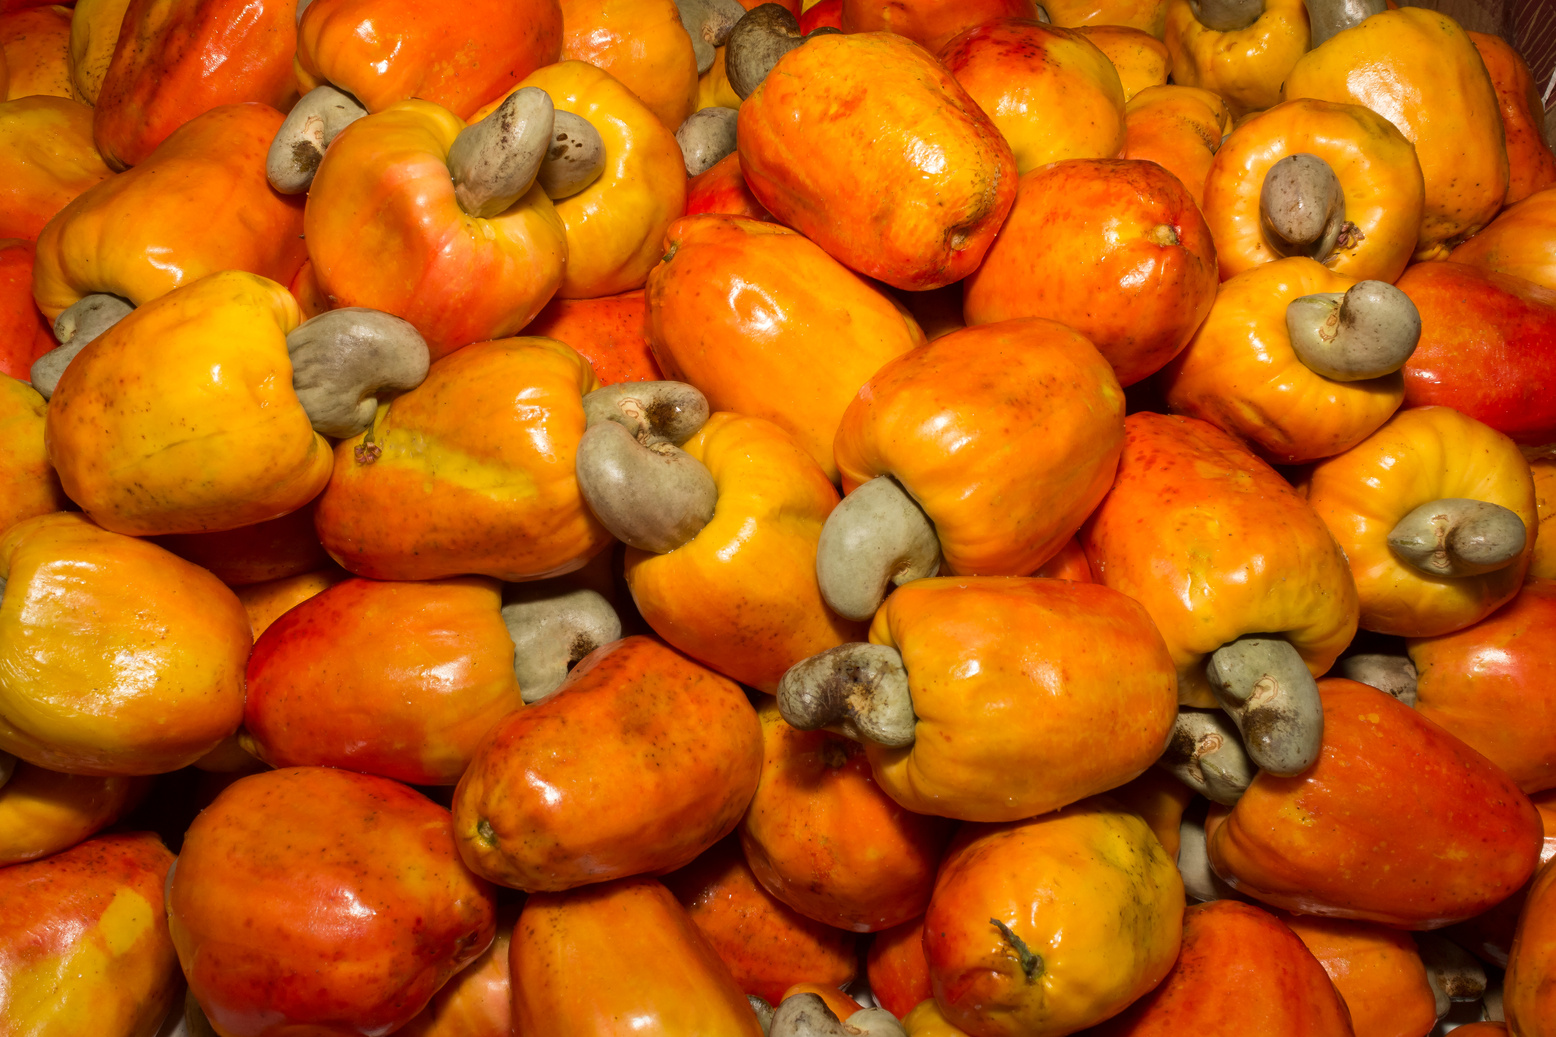
KOR 48-52
Raw cashew nut orchard harvesting with mandatory KOR sampling cut-tests.
 STAGE 02
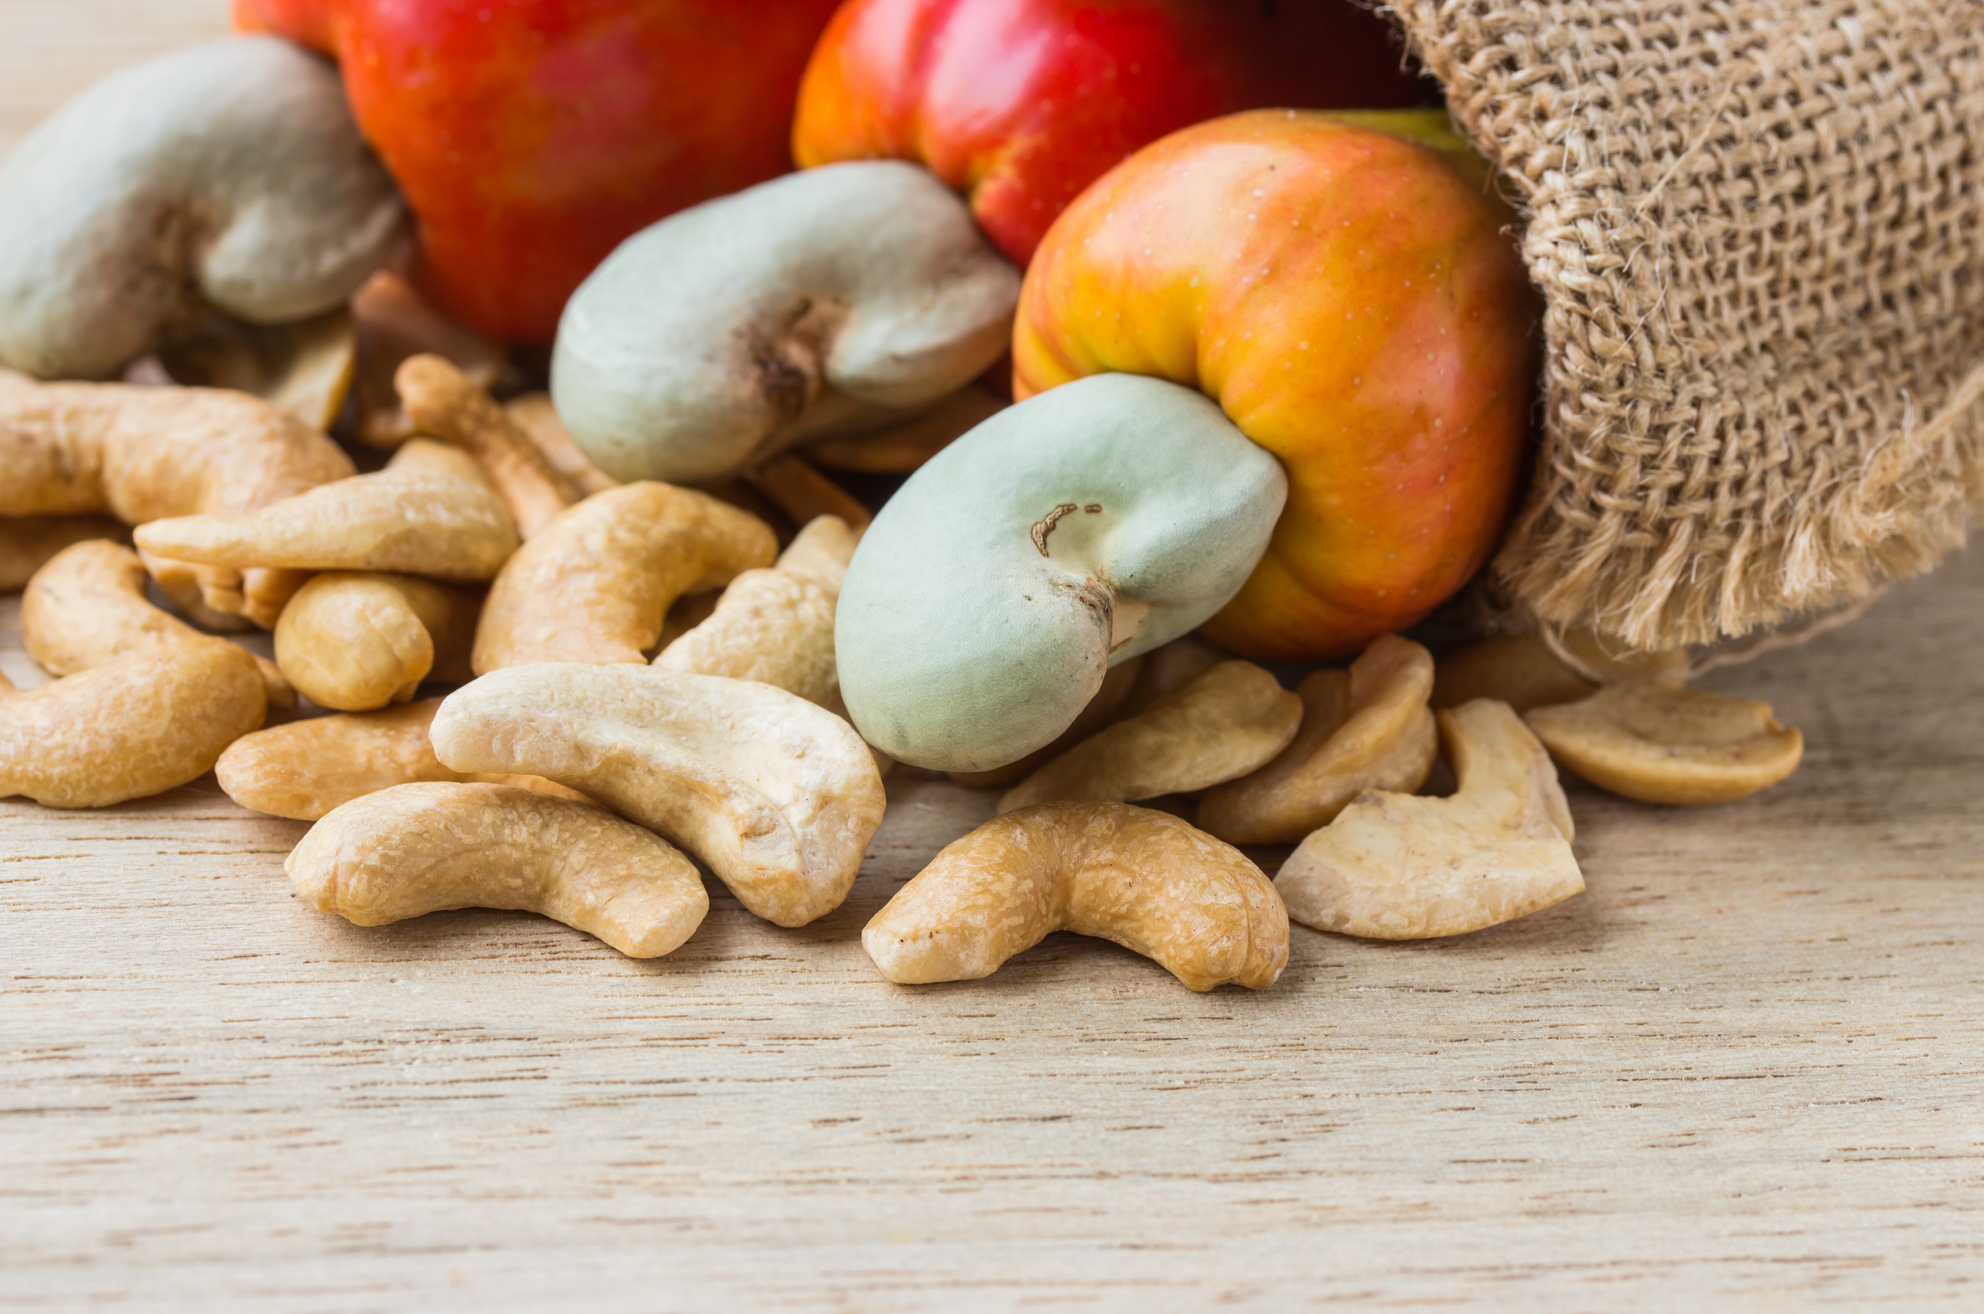
7% - 8% Moist
Vibratory destoning, debris separation, and 72-hour solar moisture conditioning.
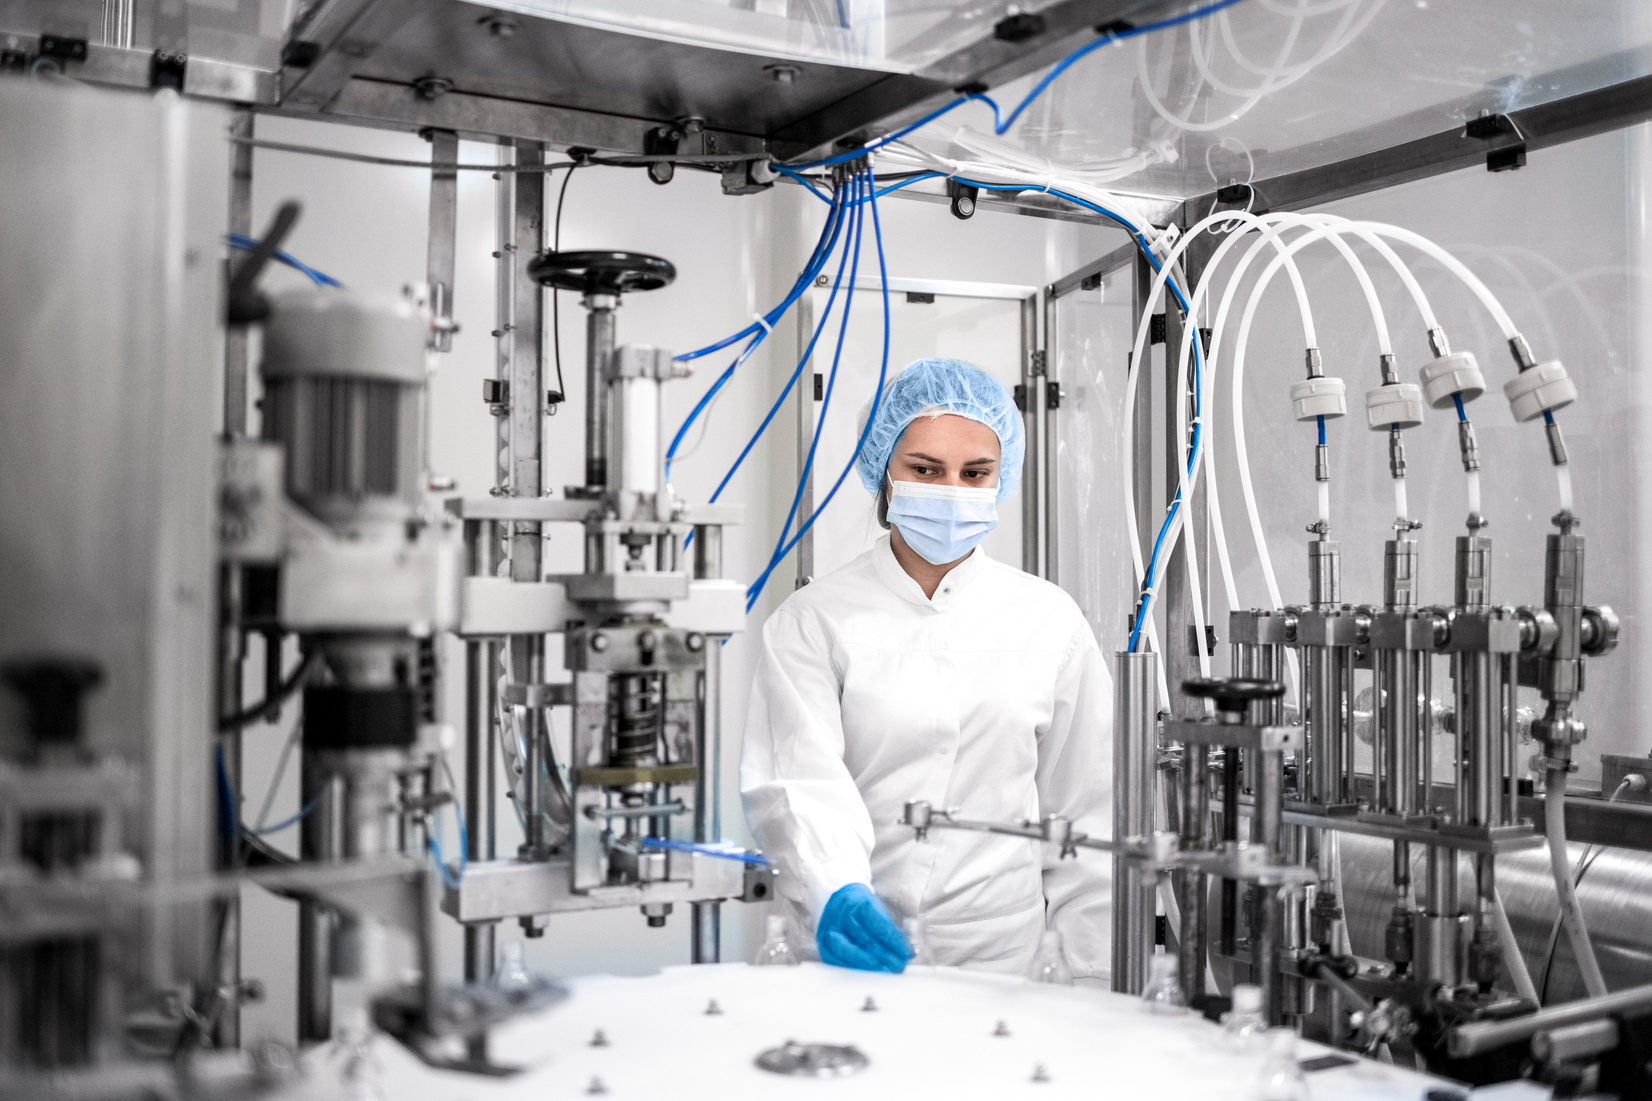 STAGE 03
90°C Steam
Micro-pressure steam tanks safely softening outer hull & isolating CNSL liquid.
 STAGE 04
>94% Whole
Dual-blade motorized cracking machines extracting intact whole cashew kernels.
 STAGE 05
70°C / 24h
Controlled 70°C hot-air desiccation loosening the reddish testa skin for peeling.
 STAGE 06
Stabilization
Controlled ambient airflow cooling to room temperature, loosening outer testa skin.
 STAGE 07
Airjet Testa
Pneumatic vortex airjets strip outer testa skin cleanly without chemicals.
 STAGE 08
12k Kernels/s
CCD cameras inspecting 12,000 nuts/sec and blasting defects with optical airjets.
 STAGE 09
W180 - W320
Thermal conditioning and precision vibrating caliper sieving into export grades.
 STAGE 10
< 5.0% Moist
Precision moisture desiccation ensuring moisture < 5.0% prior to packaging.
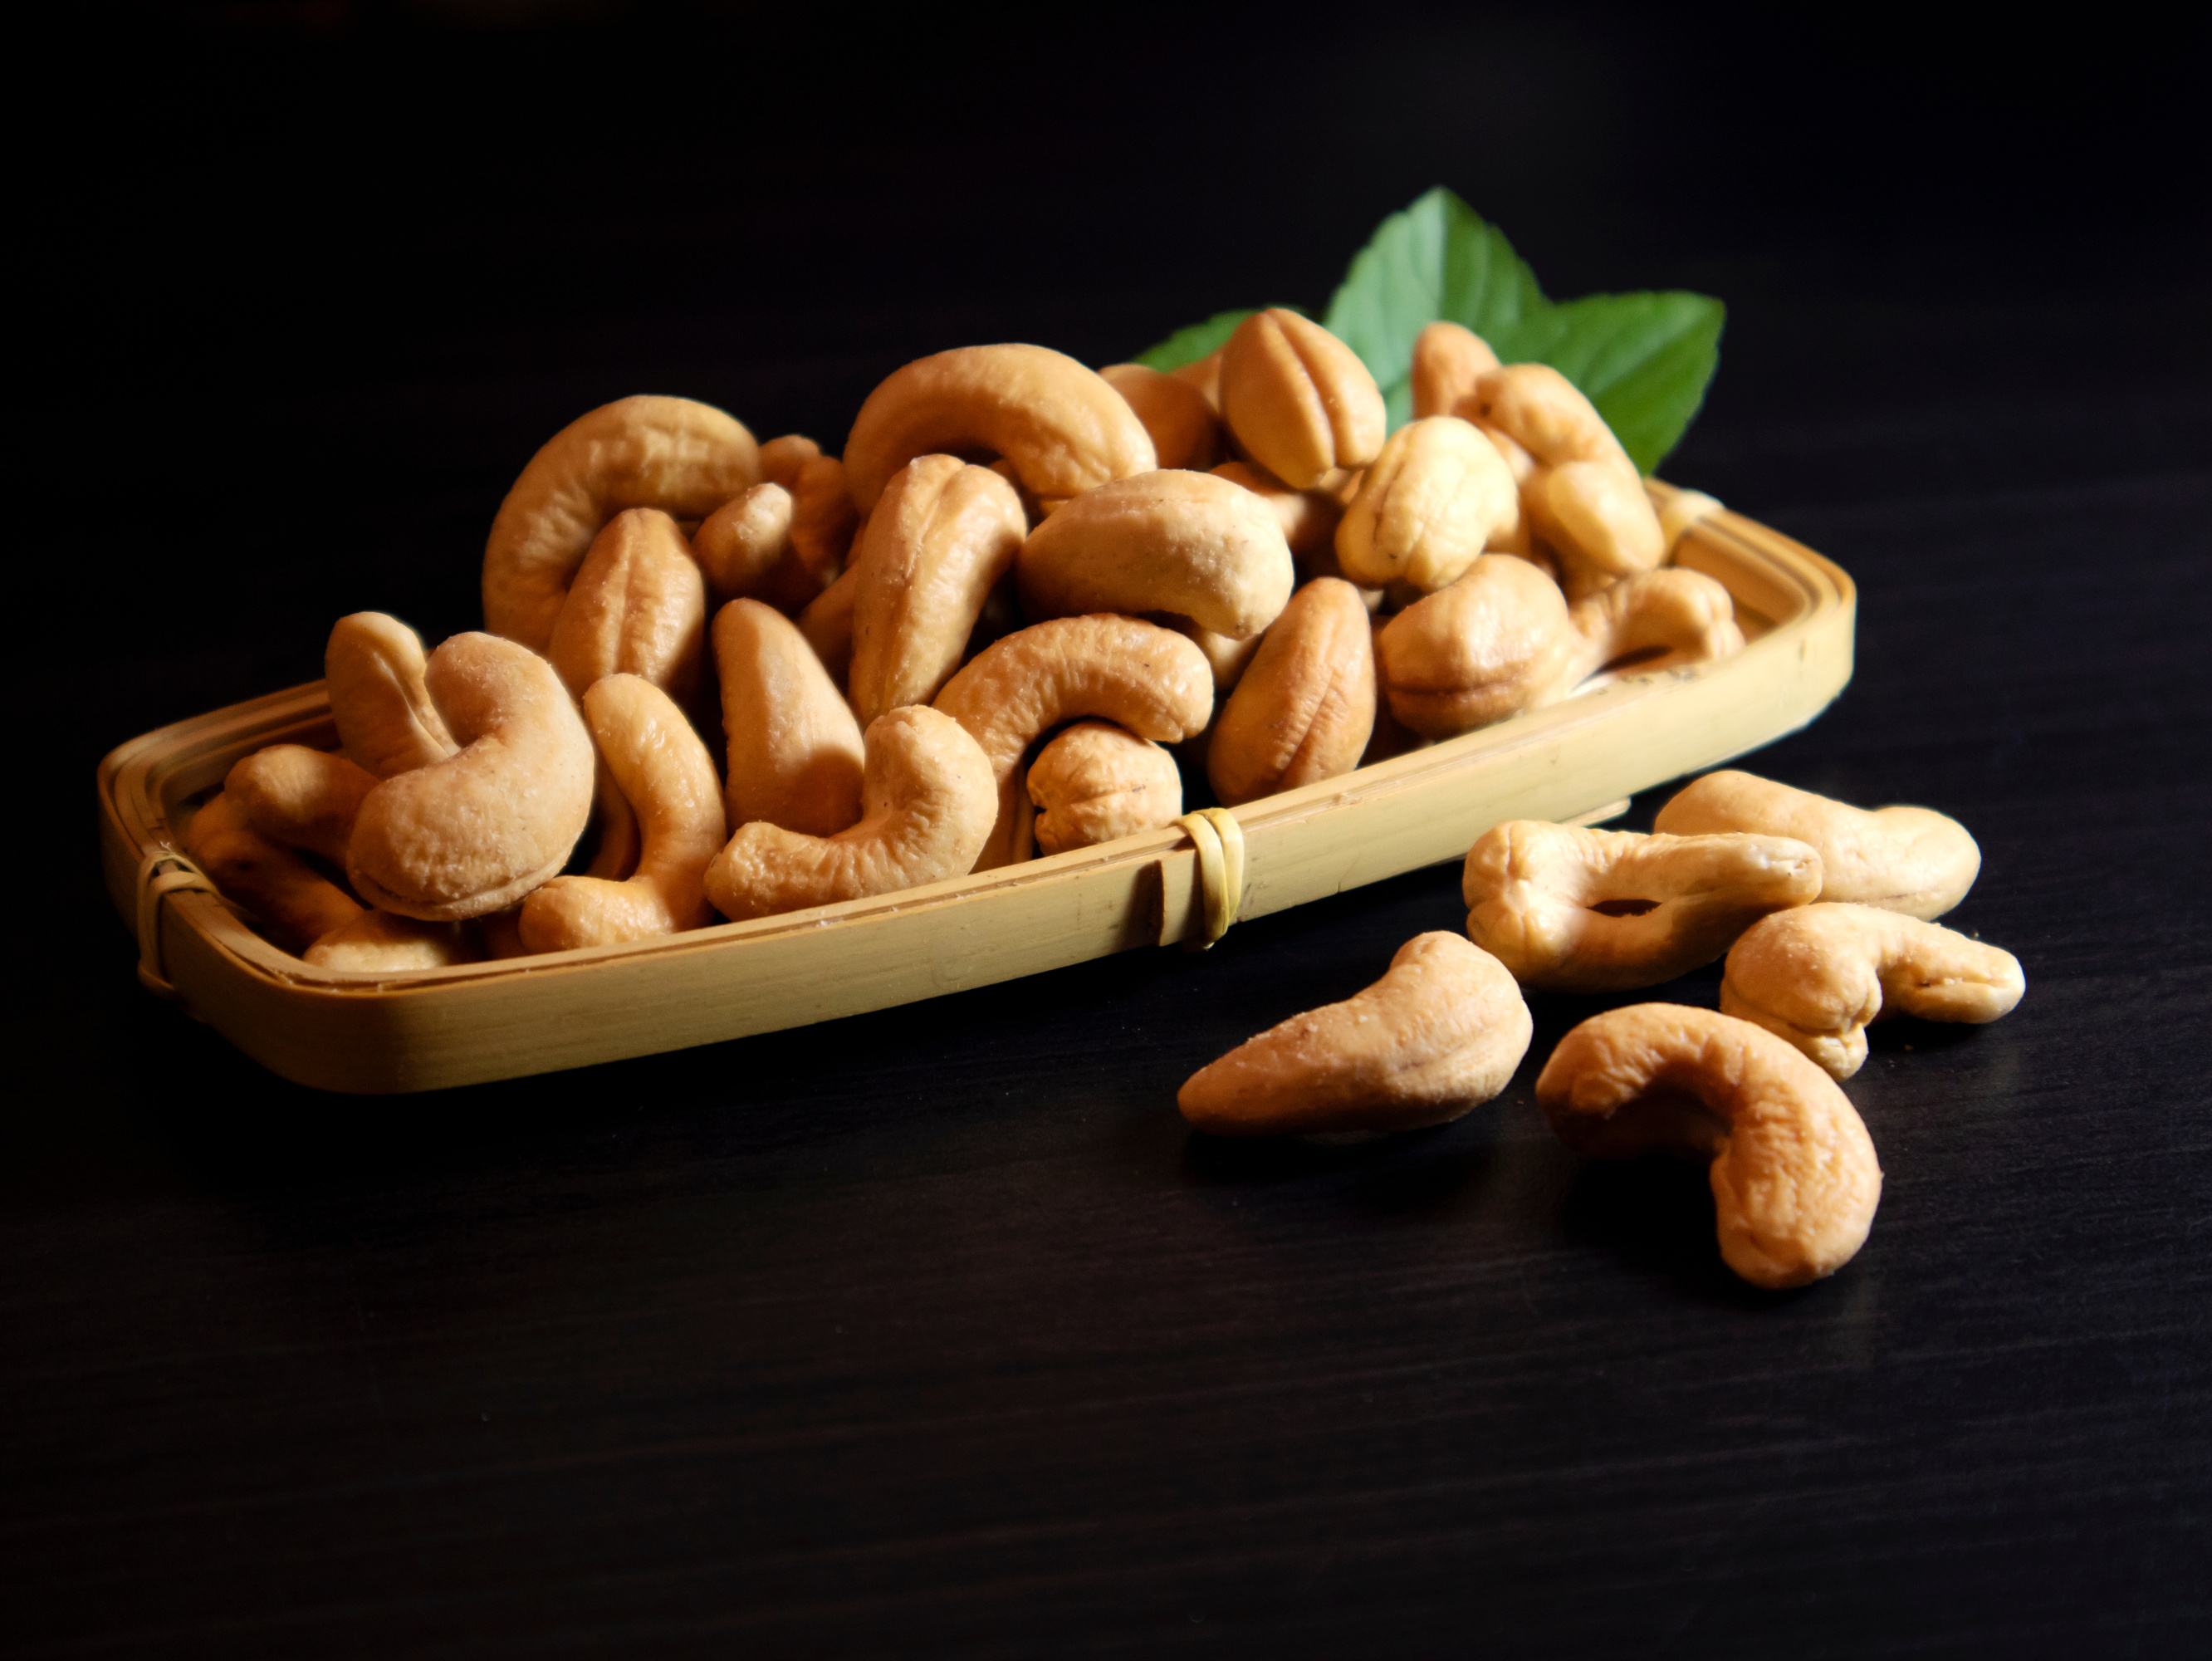 STAGE 11
N2 Flush Tins
Nitrogen backflush into 25lb tins & pouches for 24-month freshness.
From the raw cashew nut (RCN) tree harvest to hermetically sealed vacuum containers, every step is rigorously calibrated to eliminate contamination and preserve kernel wholeness.
Harvested raw cashew nuts arrive from domestic organic farms and accredited West African cooperatives with thorough out-turn (KOR) testing.
Rotary sizing drums, high-speed aspirators, and vibrating destoners extract dust, twigs, and stones before entering solar drying and thermal conditioning.
Computer-regulated steam pressure tanks soften the resilient outer shell and safely isolate corrosive CNSL liquid from the internal edible nut.
Mechanized dual-blade cutting machines crack the outer hull cleanly, delivering maximum yield of unbroken, intact whole white kernels.
Uniform hot-air circulation chambers slowly dry the kernels at 70°C for 24 hours, stabilizing moisture to exactly 5-6% so the reddish testa skin loosens.
Kernels rest in laminar airflow cooling bays for 24-36 hours, equilibrating kernel core temperature and crisping the loosened testa skin.
Specially textured soft rubber rollers combined with pneumatic vortex airjets gently strip away the outer testa without nicking or bruising the kernel.
Advanced bi-chromatic digital CCD cameras inspect 12,000 kernels per second, detecting spots and blemishes with micro-precision pneumatic ejection.
Gentle thermal heating conditions kernels for vibratory multi-deck sizing screens and illuminated artisan inspection tables classifying AFI grades (W180 - W320, Splits, Pieces).
Controlled post-grading desiccation reduces residual moisture below 5.0%, locking in crunch and shelf stability.
Atmospheric air is evacuated down to 0.5% residual oxygen and refilled with food-grade high-purity nitrogen in 25lb / 50lb tins or EVOH vacuum pouches for 24-month crisp freshness.
We provide full documentation: Phytosanitary, Certificate of Origin, Bill of Lading, and SGS/Eurofins lab reports on request.